Ceramic 3D Printing Service | Alumina, Zirconia, Silicon Carbide
 Introduction: Breaking the Geometric Limits of Traditional Ceramic Manufacturing
A ceramic 3D printing service is best used for alumina, zirconia, silicon carbide, and related engineering ceramic parts when complex geometry justifies additive forming and post-processing is planned for density, shrinkage, surface texture, and critical dimensions. Printed ceramic parts normally begin as fragile green bodies, pass through debinding and sintering, and may still need grinding or polishing before functional surfaces can be accepted. Pure additive processing is a poor fit when every face needs tight form control or when a simple dense shape can be formed or machined with less qualification risk. Buyers should define the exact ceramic system, internal geometry, wall transitions, service duty, final datums, and inspection method before asking a supplier to select the printing route.
Core Ceramic 3D Printing Technologies: Stereolithography (SLA) and Binder Jetting
Ceramic SLA, DLP, and binder jetting all create an intermediate ceramic body, but they control feedstock, support, powder removal, debinding, shrinkage, and surface condition differently. The printer name alone cannot select the route. The buyer must compare the fully processed material state, accessible finishing stock, internal cleaning path, and feature-specific inspection plan.
Ceramic SLA and DLP use a photosensitive slurry containing ceramic powder, resin, and process additives. SLA scans selected cross-sections, while DLP exposes projected areas; both create a polymer-bound green body that requires cleaning, debinding, and firing. These routes suit fine walls, small passages, insulating bodies, dental forms, and fluidic features when slurry stability and light exposure are qualified. Support witness, trapped uncured slurry, local overcure, and firing movement can still change a critical edge or channel. The drawing should separate as-sintered surfaces from faces reserved for final grinding.
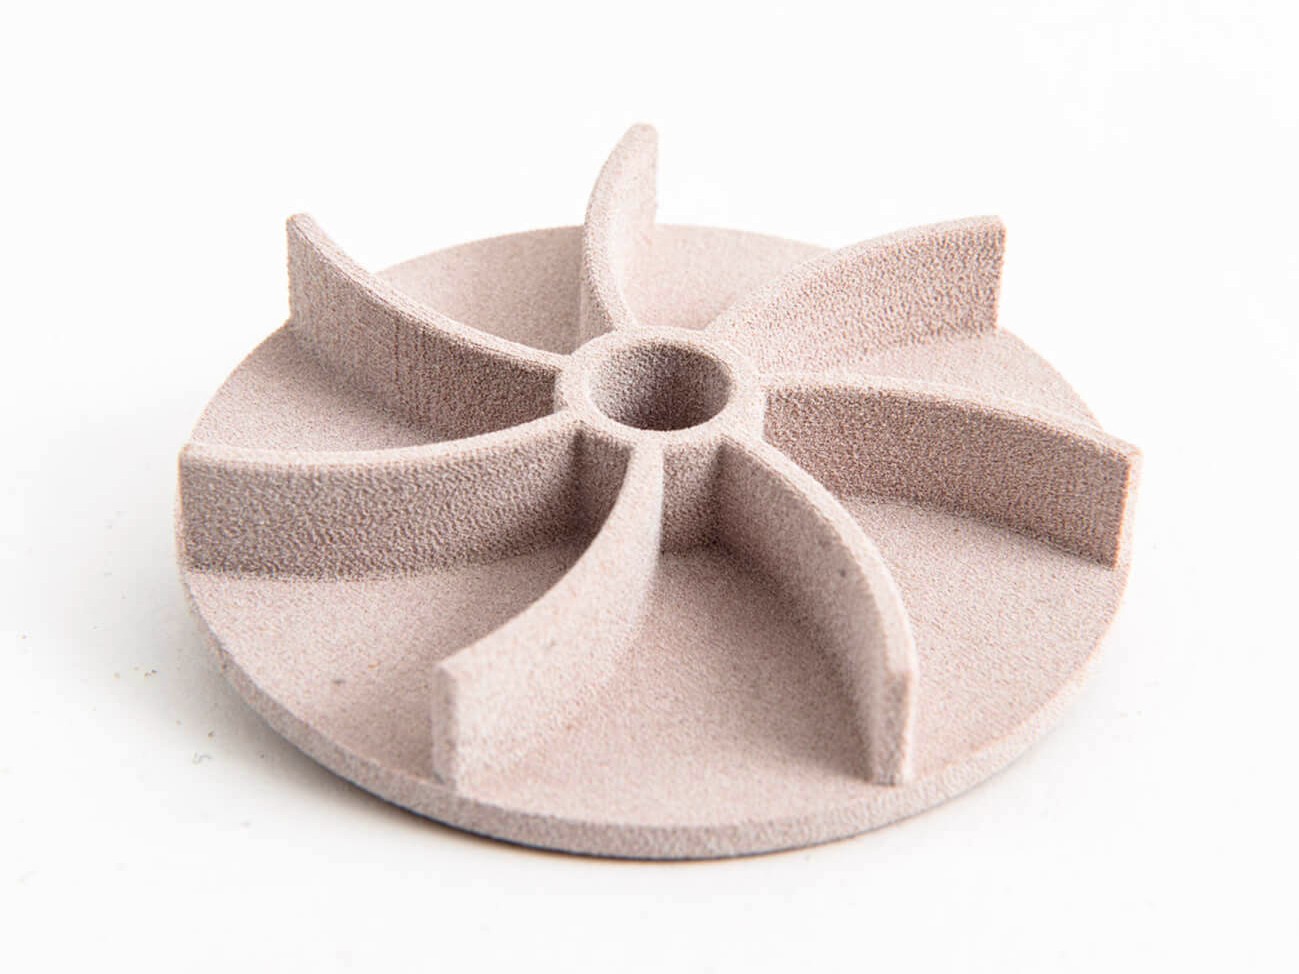
Binder jetting technology deposits liquid binder into a dry ceramic powder bed. Surrounding powder can support the shape during printing, which helps some larger forms and fragile overhangs, but the green part remains weak. Powder evacuation, binder distribution, section thickness, furnace support, and the selected sintering or infiltration route then control success. A closed channel can retain powder even when its CAD diameter looks adequate. Thick-to-thin transitions can also drive local distortion, so cleaning access and section changes need review before the build is released.
Ceramic additive manufacturing differs from metal or plastic 3D Printing because the printed geometry does not establish the final ceramic properties. Density, porosity, grain structure, phase composition, dielectric response, thermal transport, and chemical resistance can change during debinding, sintering, infiltration, and finishing. An RFQ should identify the ceramic grade or supplier system, required final state, inaccessible features, functional surfaces, allowable porosity, inspection datums, and any requirement that later grinding cannot correct.
In-Depth Analysis of Three High-Performance Engineering Ceramic Materials
Alumina, zirconia, and silicon carbide are viable ceramic additive materials for different duties: alumina commonly serves electrical insulation and wear, zirconia serves toughness-sensitive or appearance-critical parts, and silicon carbide serves demanding thermal, chemical, or wear conditions. Those are screening directions, not interchangeable grade claims. Final selection must use the specified composition, forming and densification route, surface state, geometry, environment, and acceptance tests.
Alumina ceramics are a practical starting point for electrical insulation, wear resistance, chemical stability, and thermally stable fixtures. Alumina (Al₂O₃) can suit insulators, spacers, analytical nozzles, wear guides, and fluid-handling parts when its grade and purity match the duty. Sharp internal corners, unsupported ribs, local press fits, and grinding damage can initiate fracture. The drawing should identify loaded edges, dielectric paths, sealing zones, permitted porosity, surface texture, and any datum that must be ground after firing.
Zirconia ceramics are selected when the design needs more fracture resistance than a comparable alumina route or when a dense, polishable contact surface matters. Zirconia (ZrO₂) can serve pump elements, valve seats, wear sleeves, dental forms, and small structural components. Transformation toughening depends on composition, stabilizer, thermal history, and service environment. Color, hydrothermal aging, sterilization, contact wear, and grinding heat therefore need grade-specific validation. A zirconia label by itself cannot establish shade, aging resistance, or finished-part strength.
Silicon carbide ceramics are considered for thermal transport, thermal shock, chemical stability, and severe wear. Silicon Carbide (SiC) can support heat-exchanger features, burner hardware, semiconductor fixtures, pump components, and high-temperature wear parts. Qualification must distinguish reaction-bonded or infiltrated SiC, sintered SiC, and converted material systems. Free silicon, residual porosity, secondary phases, incomplete infiltration, and machining allowance affect thermal, chemical, and sealing behavior differently. The RFQ should name the target phase and property condition instead of requesting only “3D-printed SiC.”
Five Key Advantages of Choosing Ceramic 3D Printing
Ceramic additive manufacturing earns its place when complex geometry, functional integration, or rapid design learning outweighs the qualification burden of green-body handling and thermal processing. It is strongest for low-volume, high-value parts whose drawings distinguish printed geometry from final acceptance surfaces. It is weaker for simple dense shapes, broad tight-flatness requirements, or parts that need grinding on nearly every face. In those cases, conventional forming or dense ceramic machining may carry lower accepted-part risk.
Geometric freedom for functional features is the primary reason to select ceramic 3D printing. Internal channels, porous regions, thin-wall lattices, integrated manifolds, and weight-reduced fixtures can be formed without a dedicated hard tool. The benefit survives only when the part still permits slurry or powder removal, debinding-gas escape, support removal, furnace support, and inspection access. A hidden passage that cannot be cleaned or inspected is not a manufacturable advantage, even if the printer can reproduce its CAD section.
Tooling-free, rapid iteration supports early design learning because engineers can move from CAD into the Prototyping Service stage without first committing to a pressing die or casting mold. This route adds value when the prototype verifies flow, fit, thermal exposure, insulation distance, handling, or finishing access. It adds less value when the final geometry is a washer, plate, sleeve, or spacer that a qualified forming or machining process can produce with fewer state changes.
Material performance after validation depends on powder chemistry, solids loading, binder removal, firing cycle, density, grain structure, surface state, and secondary operations. ISO 18754:2020 provides methods for density and apparent porosity of fine ceramics, while ISO 14704:2016 addresses room-temperature flexural strength of monolithic fine ceramics. Neither standard supplies a universal acceptance value for a printed part. The buyer must specify the target, specimen orientation, final surface, sampling plan, and whether a witness coupon represents the same build and furnace lot.
Functional integration with fewer joints can remove seals, fasteners, alignment operations, and assembly interfaces. A printed ceramic manifold, sensor housing, or insulating carrier may consolidate several parts into one body. The risk does not disappear; it moves toward ceramic cracking, local shrinkage, hidden blockage, post-sinter inaccessibility, or an unrecoverable datum shift. Design review should connect radii, section changes, edge loading, final machining access, and a leak, flow, dielectric, or dimensional test to each integrated function.
Support for customization and low-volume production makes ceramic additive manufacturing useful for research fixtures, medical development parts, semiconductor process tools, and specialized thermal or electrical components. For low-volume manufacturing Service or one-off work, the buyer should budget for first-article inspection and a controlled design correction. The economic case comes from avoiding tooling and learning earlier. It does not come from omitting ceramic process qualification, inspection, or reject criteria.
From “Green Body” to Dense Part: Key Post-Processing Steps in Ceramic 3D Printing
Printing establishes shape, but debinding and sintering usually decide whether a ceramic part survives and reaches its intended material state. Debinding removes resin, binder, or other organics through a qualified thermal schedule. Rapid gas generation, blocked escape paths, large section changes, weak supports, and rough handling can crack or distort the body before densification begins. Process review should therefore examine vent paths, thermal mass changes, setter contact, support witness, fragile edges, and how the part will be transferred between cleaning and the furnace.
High-temperature sintering develops density and microstructure through ceramic diffusion and grain growth. It is related only in a broad thermal-processing sense to Heat Treatment for CNC Machining; ceramic firing has different material mechanisms, shrinkage behavior, furnace-support needs, and acceptance risks. A single CAD scale factor can compensate for qualified average shrinkage, but it cannot correct local movement caused by wall transitions, setter friction, density variation, or uneven thermal mass. First-article measurement should use final drawing datums and record the material and furnace lot.
Finishing turns a fired ceramic blank into an accepted component when the drawing requires datums, bores, flatness, sealing, sliding contact, or specified surface texture. Sintered ceramics may need CNC Grinding Service with diamond tools, stable fixtures, coolant control, stock allowance, and edge protection. Grinding can correct accessible geometry, but it cannot repair hidden porosity, a blocked channel, or material missing from a distorted edge. When friction, cleaning, appearance, or sealing requires a smoother surface, CNC Part Polishing Service should be tied to a defined texture parameter, evaluation method, and final process state.
Ceramic 3D Printing vs. Traditional Ceramic Manufacturing vs. CNC-Machined Ceramics
Select ceramic 3D printing for inaccessible or rapidly changing geometry, conventional forming for repeatable geometry that justifies tooling, and dense ceramic machining for reachable precision features. A hybrid route is often strongest when one part combines hidden flow paths with ground interfaces. The decision should be made feature by feature: printing creates geometry, thermal processing establishes the ceramic state, and finishing establishes accessible datums or surfaces. Applying one tolerance expectation to all three states creates avoidable RFQ ambiguity.
Traditional ceramic manufacturing is attractive when the geometry is stable, production volume supports tooling, and the material route is already qualified. Pressing, casting, extrusion, and ceramic injection molding can be efficient for repeated parts with manageable draft, wall, and demolding requirements. Hard tooling can slow early design changes, while additive forming becomes stronger for internal channels, lattices, porous zones, and frequent iteration. Printing becomes weaker when a simple part carries broad flatness, bore, or surface requirements that later demand extensive grinding.
Compared with Ceramic CNC Machining Service, ceramic 3D printing can reduce dense-stock removal and create features that tools cannot reach. Dense machining is usually stronger for accessible precision features, controlled datum relationships, and measurable surface texture. A practical buying rule is to print the geometry that cannot be formed or machined economically, then machine only the features that control assembly, sealing, measurement, or wear. Accepted-part cost should include scrap, fixtures, inspection, and thermal-process qualification, not just printing time or raw stock.
A hybrid plan reserves Precision Machining Service for selected surfaces after sintering. Consider a ceramic microfluidic distributor with branching passages, a locating base, and two gasket lands. Printing creates the passage network, while grinding establishes the base and sealing relationship. The review should confirm slurry or powder removal before firing, remaining stock before finish grinding, and passage condition, datum position, surface texture, and leak performance afterward. The RFQ must show protected walls, grinding stock, final datums, texture callouts, and the measurement method.
Cutting-Edge Applications: How Ceramic 3D Printing Solves High-End Manufacturing Challenges
Ceramic 3D printing solves an application problem only when geometry and material duty are validated in the final process state. Heat resistance, electrical behavior, wear, chemical stability, and low mass may justify a ceramic route, but an application label does not approve the part. A buyer still needs material evidence, dimensional inspection, finishing boundaries, and a functional test. An insulating carrier, for example, may print cleanly while thin ribs crack during handling or a ground mounting face shifts the dielectric path. The acceptance plan should connect rib condition, final datum, electrical test, and service environment.
In Aerospace and Aviation, ceramic additive manufacturing can support thermal barriers, radome-related shapes, sensor housings, insulating carriers, and sacrificial cores when the material, qualification path, and inspection plan match the risk. Vibration, pressure, thermal cycling, impact, and rotating duty require different validation from a handling fixture or demonstrator. The RFQ should provide service temperature, atmosphere, load path, dielectric requirement, allowable flaws, traceability needs, and whether destructive tests may use representative specimens.
In the Medical Device sector, zirconia and alumina can be relevant for dental forms, insulating components, wear interfaces, guides, and instrument carriers, but patient-contact use changes the evidence requirement. Manufacturing feasibility does not establish biocompatibility, cleanability, sterilization compatibility, color conformity, or regulatory suitability. Those requirements need the exact ceramic system, final surface, cleaning route, intended contact, and applicable validation plan. A non-contact prototype and a released implant cannot share the same acceptance argument.
In Industrial Equipment, projects involving silicon nitride (Si₃N₄) or other engineering ceramics may target wear guides, insulating fixtures, valve elements, handling tools, chucks, and corrosion-resistant flow components. The buyer should state the chemical environment, contact load, cleaning cycle, temperature change, allowable leakage, and wear limit. A part can meet nominal geometry yet fail because density, edge condition, surface texture, or the inspection datum was never connected to service.
Neway’s Ceramic 3D Printing Capabilities and Commitment
A defensible supplier workflow connects material selection, printable-geometry review, green-body handling, debinding, sintering, post-sinter machining, and inspection before production release. The ceramic system should be selected before the printer route is fixed because alumina, zirconia, silicon carbide, silicon nitride, and aluminum nitride respond differently to firing, grinding, thermal cycling, moisture, and surface finishing. The review should identify inaccessible features, trapped material, critical edges, planned stock, datum transfer, destructive-test coupons, and final measurement access while CAD changes are still inexpensive.
A practical One-Stop Service, for ceramic additive work should connect DFM findings to the material route, thermal schedule, finishing allowance, inspection record, and release decision. High-thermal-conductivity ceramics such as Aluminum Nitride (AlN) also require attention to electrical insulation, surface contamination, moisture sensitivity, and machining damage. ISO/ASTM 52901:2017 provides a framework for defining purchased AM-part requirements, but it does not assign a ceramic capability. The RFQ should include native CAD, final drawings, material system, density or porosity target, critical dimensions, texture callouts, datums, quantity, service conditions, sampling, first-article deliverables, and reject criteria.
Conclusion: Opening a New Chapter in High-Performance Ceramic Part Manufacturing
Ceramic 3D printing is the right route when alumina, zirconia, silicon carbide, or another qualified ceramic must carry geometry that conventional forming or dense machining cannot create efficiently. It is not the default route for every custom ceramic part. Green-body fragility, binder removal, firing distortion, residual porosity, inaccessible surfaces, edge damage, and post-sinter stock determine whether the design becomes a repeatable component or remains a prototype.
Release the RFQ after each feature has a manufacturing state and an acceptance method. Mark geometry as printed, cleaned, debound, sintered, ground, polished, or untouched; then identify its datum, tolerance, texture, material or phase requirement, service exposure, and test method. Ask the supplier to return the proposed route, machining stock, inaccessible risks, first-article plan, sampling, and evidence for every critical function. If those inputs are not mature, use a prototype lot to qualify shrinkage, cleaning, finishing access, and inspection before requesting production pricing. That sequence gives procurement a measurable basis for choosing pure additive, conventional forming, dense ceramic machining, or hybrid manufacturing.
FAQs
Can ceramic 3D printed parts match the density and strength of sintered ones?
Can zirconia ceramics be colored (like tooth shades) after 3D printing?
What maximum build size and accuracy are currently achievable in ceramic 3D printing?
Is silicon carbide ceramic 3D printing mature, and what challenges remain?
For ultra-precise ceramic parts, is pure 3D printing or hybrid manufacturing better?