Mass Production Quality Control for CNC Machined Parts: Consistency, Inspection, and Cost Control
Mass Production Quality Control for CNC Machined Parts: Consistency, Inspection, and Cost Control
Mass-production quality control for CNC machined parts should connect the released product definition, process controls, measurement evidence, traceability, and reaction plan in one risk-based control system. The goal is consistent accepted parts across recurring lots, not the largest possible inspection count. Buyers should define critical characteristics, material and final-state requirements, control frequency, lot identity, change authority, and release evidence before routine supply begins. Each control needs a failure trigger and containment boundary. If the measurement system is unsuitable, the process changes without approval, or a critical trend crosses its limit, the affected output should be held. Production resumes only after the cause, containment, corrective action, and revalidation evidence meet the agreed release rule. The control plan should distinguish setup approval, process continuation, and shipment release because they answer different questions. It should also define how records connect each accepted lot to its machine, fixture, tool condition, material, outside process, inspection status, and revision.
This scope gives buyers evaluating mass production services a practical way to compare quality plans and their cost. A machine list, quality certificate, or conforming first sample cannot prove recurring lot control by itself. The supplier response should show how incoming lots, setup approval, tool and fixture condition, in-process checks, outside processing, final acceptance, nonconformance, and shipping release remain linked to the same revision. Inspection cost must use the same basis as production cost. A cheaper plan may simply omit required evidence, while an expensive plan may repeat measurements that do not control product risk. The buyer needs a justified balance, with assumptions visible in the RFQ and control plan.
Why Quality Control Is Different in Mass Production
Quality control is different in mass production because the acceptance decision must remain reliable across time, lots, tools, fixtures, material changes, operators, and delivery cycles. A sample inspection answers whether one submitted part met the stated requirements. Recurring production must also demonstrate that the approved route can detect drift, isolate suspect output, preserve traceability, and recover without confusing revisions or lots. The control system therefore needs four evidence layers: product conformity, process condition, measurement suitability, and lot release. Missing one layer creates a blind spot. Accurate measurements cannot rescue an uncontrolled revision, and a stable process trend cannot prove conformity when the gauge or datum setup is wrong. Recurring production also needs change control for programs, tools, fixtures, measurement methods, outside-process sources, and parallel equipment. Each change should identify affected characteristics, required validation, approval authority, and the first output that can be released under the new condition.
Mass production also changes the economics of quality. Prevention work includes released files, process planning, fixture qualification, measurement planning, and operator instructions. Appraisal work includes first-piece, in-process, final, audit, and receiving checks. Internal failure includes scrap, rework, sorting, lost machine time, and delayed lots. External failure can include line stops, returns, field containment, or damaged trust. Reducing appraisal without stable prevention can increase total cost, while measuring every feature on every part can create delay without controlling the important risks. The correct plan places controls where variation begins, then uses results and reaction rules to protect the buyer's functional requirements.
Key Quality Control Points in CNC Mass Production
Key CNC mass-production controls should be defined as release gates from incoming material through shipment. Each gate needs a controlled input, objective evidence, known failure mode, and action owner. The evidence must reflect the actual machine, fixture, material state, measurement method, outside process, and lot being released. A report from another revision or route can support learning, but it does not approve the current output. Buyers should decide in advance which failures stop production, which require containment, and who can authorize a deviation or restart. The control plan also needs a named owner, approval date, revision, and review trigger. Reviews should follow product or process changes, repeated nonconformance, measurement disagreement, new production streams, or evidence that the current frequency no longer matches risk. Open actions need closure evidence rather than a note that they will be monitored later.
Quality Gate | Evidence, Failure Mode, and Reaction |
|---|---|
Incoming material and lot identity | Match grade, condition, stock form, certificate, and heat or batch identity to the released requirement. Substitution or mixed identity can change machining response and traceability. Quarantine material until the discrepancy receives engineering and buyer disposition. |
Released setup and first piece | Verify revision, program, fixture station, datums, tools, offsets, and specified characteristics before the run. A conforming part made from the wrong setup is not valid approval. Hold production until setup evidence and required first-piece results agree. |
In-process tool and fixture condition | Monitor affected features against tool use, offset, locator condition, and clamp sequence. Wear or movement can create drift before final inspection. Stop, identify the last-known-good check, contain suspect output, and requalify after correction. |
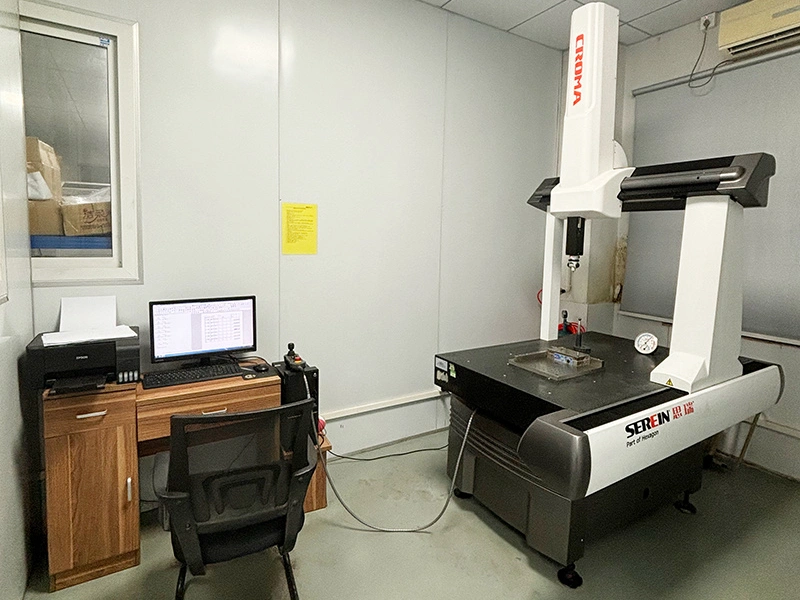
Measurement system and method | Confirm resolution, calibration status, datum simulation, fixture, environment, software, and operator method for the characteristic. Poor correlation can create false acceptance or rejection. Resolve method disagreement before using results for lot release or capability claims. |
Final-state and outside-process acceptance | Inspect dimensions, finish, masking, appearance, cleanliness, and identification after heat treatment, coating, passivation, or other required processing. Machining-stage conformity can be lost later. Isolate the processed lot until final-state evidence passes. |
Nonconformance and containment | Record requirement, actual result, affected lot range, disposition authority, rework route, and reinspection. Vague containment can release mixed or unverified parts. Preserve status and traceability until an approved disposition closes every affected unit or lot. |
Lot release and shipment | Confirm required records, quantity, revision, labels, packaging, segregation, and delivery identity before shipment. Damage or lot mixing can invalidate accepted parts after inspection. Hold the shipment when records, protection, or identity are incomplete. |
These gates extend the general methods used for quality control in CNC machining into a recurring control plan. Drawing and contract requirements remain the acceptance source. If the drawing invokes ASME Y14.5, measurement must reproduce its specified datum and geometric-tolerance framework. Customer-required sector packages should be identified in the RFQ rather than assumed. The buyer should also define the lot, frequency, and reaction rule behind any sampling plan. A named standard or form has value only when its scope, method, responsibility, and release use are clear.
How Batch Consistency Is Maintained
Batch consistency is maintained by controlling the causes of variation and reacting before they create an accepted nonconforming lot. The released route should define operation order, datum transfers, workholding, tool strategy, deburring, outside processing, and final acceptance. The control plan should identify which characteristic can move when each cause changes. Tool-life monitoring needs a check tied to the affected feature and a limit tied to containment. Fixture maintenance needs locator and clamp checks plus verification after unclamping. Material-lot changes need identity and, when risk requires it, confirmation that distortion or cutting behavior remains within the approved process response.
Measurement data must also be interpreted within its conditions. A trend is meaningful only when the same characteristic, method, datum setup, and process stream are compared. Capability indices should not be quoted without stable data, specification limits, subgroup logic, and a suitable measurement system. If the buyer requires an AIAG MSA or SPC study, the parties should agree on the current manual, study design, sampling, and acceptance use. Those methods are not universal defaults for every CNC order. Separate machines, fixtures, cavities, or shifts should not be pooled merely to create a larger data set. Stratify the results until equivalent behavior is demonstrated, and preserve stream identity in the reaction plan. When a signal exceeds its limit, the plan should stop or contain the defined process stream, not merely adjust an offset and continue without reviewing affected output.
Consider an illustrative 17-4 PH H900 actuator shaft with a turned bearing journal, milled keyway, runout requirement, and final passivation. The journal and runout depend on the defined datum setup, chucking condition, tool state, and unclamped part. A recurring-lot plan could track journal size and runout at setup approval and selected in-process points, while preserving tool and fixture identity. It should verify the final surface and identification after passivation. If a parallel machine or replacement fixture is introduced, the buyer should require equivalent-route evidence before combining results. This scenario shows the discipline expected in precision machining; it is not a Neway customer case or a universal control frequency.
Inspection Reports Commonly Required for Mass Production Orders
Mass-production inspection records should answer a release question, not exist only because a template is available. The buyer should specify which records are required, which characteristics they cover, how often they are produced, and whether they approve setup, process continuation, or shipment. Reporting scope depends on drawing, contract, industry, risk, and process history. A full dimensional layout, CMM output, material certificate, or capability study is not automatically required for every lot. Conversely, a certificate of conformance cannot replace the underlying measurements or traceability when the contract calls for them. Records should also state retention, correction, access, and correlation rules when these affect audits or receiving. If supplier and buyer results disagree, the parties need an agreed method to preserve the lot while they compare datum setup, equipment, environment, software, and calculation.
Quality Record | Scope, Limitation, and Buyer Use |
|---|---|
Ballooned dimensional record | Links reported results to released drawing characteristics and method. It supports setup or lot approval only for the identified revision and route. The buyer should resolve omitted, ambiguous, or mismatched features before release. |
First article report | Documents the first production configuration when contractually required. AS9102C applies only when the customer or aerospace contract calls for it. Define report scope and re-accomplishment triggers rather than labeling any first-piece sheet as FAI. |
Material and heat-lot record | Connects certificate, grade, condition, stock, and lot to released parts. A certificate without part-to-lot identity cannot support traceability. Hold mixed or unlinked material until the chain is restored or dispositioned. |
CMM or gauge result | Shows measured features with the applicable method, datum setup, units, and equipment identity. Output does not prove suitability by itself. Use the record only after correlation, calibration, and acceptance questions are closed. |
Process or capability record | Connects a characteristic to time, lot, tool, fixture, or process stream. Capability values require stable data and suitable measurement. The buyer should reject unsupported indices and request the underlying study conditions. |
Outside-process and final-state record | Confirms source, lot, specification, processing status, and required final checks. A supplier certificate cannot show every finished-part effect. Verify dimensions, finish, masking, appearance, or cleanliness after processing as specified. |
Lot release and NCR summary | Identifies accepted quantity, revision, traceability, open deviations, rework, and shipment status. A pass summary that omits unresolved nonconformance can mislead receiving. Release only after approved dispositions and reinspection are complete. |
Buyers can use these records to distinguish evidence from presentation when comparing reliable CNC machining shops. A polished report package is useful when its revision, lot, characteristic, method, and approval status are traceable. It is weak when the report cannot be connected to the shipped parts or accepted route. The RFQ should state retention, language, electronic format, approval, and delivery timing when those details affect receiving or regulatory work.
Balancing Inspection Cost and Production Efficiency
Balance inspection cost and production efficiency by applying controls according to feature risk, process knowledge, and failure consequence. Start with the functional and contract requirements, then map each one to its variation source and detection method. Controls at the source can prevent more cost than repeated final sorting. A tool-condition check can protect a wear-sensitive bore, while a fixture verification can protect datum-related geometry. Final inspection still confirms shipment requirements, but it should not carry the entire burden of process control. Any proposal to reduce inspection should state the evidence, affected features, new frequency, reaction rule, and buyer approval needed. Review the saving against added failure exposure, not against inspection hours alone. Include expected scrap, rework, containment, report preparation, delayed release, and receiving work when those costs can move between supplier and buyer.
Sampling is not simply a cheaper substitute for full inspection. The plan needs a defined lot, selection method, acceptance criteria, and response to a failed sample. ISO 2859-1 may support attribute sampling when the contract and application make it appropriate, but it does not establish process capability or replace critical-feature control. Variable data, destructive tests, safety characteristics, or unstable processes can require different methods. A failed sample should trigger the agreed lot disposition, containment, and review of the process stream that produced it. Repeatedly increasing the sample after a failure is not a substitute for finding the cause. Buyers should define how the plan returns to its normal frequency after corrective action and verified stability. They should also include the cost of containment, line interruption, reinspection, and delayed release when comparing plans. A modest prevention or in-process cost can be economical when it reduces a much larger failure exposure.
Equipment and system labels require the same evidence boundary. The linked topic on ISO-certified CMM quality assurance can help frame questions about certificate scope, equipment, calibration, method, and reporting, but certification does not prove part-specific capability. A PDCA quality system can organize corrective action and recurrence prevention, yet the current issue still needs a defined cause, containment, action owner, effectiveness check, and re-release evidence. Buyers should request the evidence relevant to their revision, process, and lot.
Build a Quality-Control Package for Recurring CNC Supply
Build the quality-control package before recurring supply begins. Provide released CAD and drawings, material and final-state requirements, critical characteristics, annual demand, release-lot cadence, acceptance method, traceability, reporting, packaging, delivery, and change-notification rules. Ask the supplier to return a proposed route, control points, measurement methods, sampling assumptions, reaction plan, capacity constraints, outside-process controls, and record list. Separate mandatory contract evidence from supplier-proposed controls. Request the expected prevention, appraisal, containment, and reporting costs as separate assumptions when they materially affect price. Define which records arrive with each lot and which remain available on request or audit. Require a revision-controlled approval matrix so temporary containment cannot silently become the permanent production method. Identify who can approve deviations, rework, inspection changes, process transfers, and restart after containment. This package lets engineering, quality, and procurement evaluate the same risk and cost basis.
Buyers can place that package in the commercial context of mass production services without treating the service page as proof of project capability. Request evidence for the actual part, revision, material state, route, planned rate, inspection burden, outside process, and shipment cadence. Compare recurring and nonrecurring quality costs separately, and expose all assumptions behind sampling or reporting reductions. The correct award or release decision follows the evidence: approve the plan, approve with explicit containment and closure actions, or hold until critical gaps are resolved. That decision protects consistency while keeping inspection effort tied to real product risk.
FAQ