How to Evaluate CNC Machined Part Manufacturers for Quality, Capacity, and Lead Time
Computer numerical control (CNC) suppliers qualify as strong cnc machined part manufacturers when they can prove three things: the planned process fits the part, the quality evidence supports the drawing, and available capacity can meet a credible lead time. That proof must reflect the exact geometry, material grade and condition, critical characteristics, finishing route, order stage, and inspection requirements. A broad machine list or one acceptable sample is not enough because either can hide workholding, measurement, outside-processing, or repeatability limits. Before awarding work, the buyer should request a process route, characteristic-level inspection plan, constraint-based schedule, and representative release evidence. The evaluation should also define which deviations require buyer approval.
A low quote or short delivery promise cannot replace evidence that the proposed route will work under the intended order conditions. Evaluate scope first, then compare design-for-manufacturability (DFM) findings, quality controls, usable capacity, schedule dependencies, and recovery plans. Reliable CNC machining services connect drawing review, programming, workholding, machining, deburring, outside finishing, inspection, nonconformance control, and shipment release. The buyer's next action is to issue the same controlled request for quotation (RFQ) package to each candidate and score only documented, comparable responses. Unresolved drawing conflicts, unapproved substitutions, unsupported measurement methods, or unnamed process owners should stop an award until they are closed.
What Buyers Really Mean by CNC Machined Part Manufacturers
A CNC machined part manufacturer is the organization accountable for converting the controlling drawing and model into conforming, released parts through a defined production route. The route may include turning, milling, drilling, boring, grinding, deburring, heat treatment, coating, cleaning, inspection, and packaging. The useful distinction is accountability, not the length of the process list. A manufacturer must identify who owns every internal and outside step, which revision governs, how critical features are protected between operations, and what record releases the part. Procurement teams should therefore evaluate the proposed route for their actual part rather than accepting a general list of industries, machines, or materials.
The supplier workflow should begin with a contract and manufacturability review of the drawing, model, revision, units, material, finish, quantity, and acceptance requirements. It should then connect stock verification, programming, fixture and datum planning, operation sequence, in-process checks, deburring, outside processing, final-state inspection, packaging, and delivery. Changes to material, setup, program, inspection method, or outside source need a defined review path when those changes can affect approved requirements. A candidate that cannot show this chain may still machine an acceptable first piece, but the buyer has little evidence that later lots will follow the same controlled route.
The Main Factors Buyers Should Compare
Machining Capability
Machining capability is the demonstrated fit between the part's dominant features and the supplier's proposed equipment, workholding, setup, tooling, and inspection access. A prismatic housing may depend on multi-face datum transfer and free-state stability after unclamping. A turned shaft may depend on chucking strategy, slenderness control, concentric features, and thread verification. Ask the candidate to mark the setup sequence, datum references, difficult tool access, special tooling, and features that move between operations. Machine travel or axis count only shows that a setup may be possible; it does not prove finished-part tolerance. The buyer should release a representative trial only after the route explains how critical relationships survive each repositioning and how they will be checked.
Material Range
Material capability means controlled experience with the specified grade, condition, stock form, and required downstream treatment, not a claim that the shop machines an entire alloy family. Aluminum, stainless steel, carbon steel, brass, bronze, titanium, nickel alloys, and engineering plastics create different chip, heat, tool-wear, burr, distortion, and handling risks. The RFQ should state the exact designation, temper or heat-treatment condition, stock form, certification or traceability requirement, and whether substitution needs written approval. Request the proposed cutting and workholding considerations only to the level needed for qualification. A supplier that answers with a different but unnamed grade, or treats material condition as interchangeable, has not resolved the material risk.
Precision Capability
Precision capability is proven by a feature-specific manufacturing and measurement plan, not by a shop-wide tolerance number. American Society of Mechanical Engineers (ASME) Y14.5 provides rules for stating and interpreting geometric dimensioning and tolerancing (GD&T) on drawings and digital product definitions. Citing the standard does not prove that a supplier can meet one requirement. For a bore, position, flatness, profile, sealing face, or thread, ask which datum setup controls machining, which method verifies acceptance, and whether the method can access the feature in its specified state. A coordinate measuring machine's resolution, a machine's positioning specification, and a finished-part tolerance are different quantities. Where risk or customer requirements justify it, request measurement-system evidence for the selected method, fixture, operator, and environment before relying on inspection data.
Lead-Time Stability
Lead-time stability is the supplier's ability to meet a dated route through its actual constraint, not the shortest number in a quotation. Break the schedule into material procurement, programming, tooling and fixture readiness, machining, outside processing, inspection, packing, and transport. Then ask which step controls completion, how much approved work is already ahead of the order, and who owns recovery if that step slips. Spare machines do not solve a bottleneck in programming, a unique fixture, inspection throughput, heat treatment, or coating. A credible commitment identifies dependencies, decision dates, buyer inputs, and a recovery trigger; an aggressive date without those details is only an assumption.
Quality Control
Quality control is adequate when the supplier can link each critical characteristic to a production control, a suitable measurement method, an acceptance record, and a reaction plan. A quality-management certificate may establish system context, but its scope and status do not replace part-level evidence. Review incoming material identification, first-article content, in-process checks, final inspection, calibration status, nonconformance segregation, corrective action, and change notification. The U.S. National Institute of Standards and Technology (NIST) describes metrological traceability as an unbroken chain of calibrations to specified reference standards. Each organization remains responsible for establishing traceability of its results. For repeat production, require statistical monitoring only where the characteristic and customer requirement make it meaningful. One conforming first article cannot by itself demonstrate a stable recurring process.
Evidence Category | Evidence to Request | Acceptable Signal | Do Not Advance If |
|---|---|---|---|
Geometry and route | Setup, datum, tooling, and inspection-access plan | Critical relationships remain controlled between operations | The answer is only a machine list |
Material control | Exact grade, condition, stock form, and traceability route | Substitutions require documented buyer approval | Grade or condition remains an assumption |
Quality evidence | Characteristic, method, acceptance record, and reaction plan | Measurement fits the feature and final state | Equipment resolution is offered as tolerance proof |
Usable capacity | Constraint step, committed load, owner, and recovery trigger | The schedule includes every internal and outside step | Machine count substitutes for a capacity plan |
Delivery and change control | Dated milestones, dependencies, escalation, and change notice | Delay and route-change decisions have named owners | Critical dependencies or outside sources are unnamed |
Prototype, Low-Volume, and Mass Production Require Different Strengths
Prototype, low-volume, and mass-production orders require different release evidence because the buyer's decision changes at each stage. A prototype can test geometry and function, but it may not represent recurring fixtures, cycle control, inspection frequency, or supply-chain constraints. Low-volume orders test controlled repetition and revision handling. Recurring production adds constraint capacity, tool-life control, lot traceability, change management, and recovery planning. The buyer should define the next decision before ordering the current stage and prevent a successful sample from becoming automatic approval for a different production route.
Prototype Orders
Prototype qualification should answer whether the design, material, feature relationships, and proposed measurement methods are workable under known conditions. A supplier supporting prototyping should identify every departure from production intent, including soft fixtures, selected stock, manual correction, alternate finishing, or expanded inspection. Record which findings require drawing revision, approved deviation, another build, or functional testing. The prototype is useful only when its configuration, process exceptions, inspection results, and failure disposition are traceable. Do not treat a hand-finished sample as evidence of repeat capability unless the same finishing step is planned, controlled, and acceptable in later orders.
Low-Volume Orders
Low-volume qualification should prove that the approved design can be repeated through a controlled route without hiding variation through sample selection or exceptional rework. In low-volume manufacturing, compare at least the controlling revision, material lot, setup and fixture version, program revision, inspection method, outside-process source, nonconformance handling, and delivery record across releases. A small batch can reveal datum shift, tool-wear effects, burr growth, finishing variation, and measurement disagreements that one sample misses. Release the next order only after causes and corrective actions from the trial are closed under representative conditions.
Mass Production Orders
Mass-production qualification should demonstrate that the intended route, staffing, equipment family, workholding, inspection throughput, and outside services can support recurring demand without uncontrolled changes. A supplier prepared for mass production should define tool-life decisions, in-process reaction rules, lot identification, schedule escalation, approved alternates, and notification before route changes. When automotive or customer-specific requirements invoke the production part approval process (PPAP), use evidence from the defined process under actual production conditions and the intended output rate. Unrelated CNC purchases do not acquire a PPAP obligation by default. Award recurring volume only after the representative route meets technical, quality, capacity, and delivery gates together.
Order Stage | Buyer Decision | Minimum Release Evidence | Hold Point |
|---|---|---|---|
Prototype | Is the design and proposed route workable? | Configuration, exceptions, inspection, and functional disposition | Unrecorded manual correction or unresolved failure |
Low-volume | Can the approved route repeat across releases? | Revision, lot, route, variation, and corrective-action records | Selected samples hide route or measurement variation |
Mass production | Can recurring demand be controlled and recovered? | Constraint capacity, reaction rules, traceability, and change control | Production evidence uses a nonrepresentative process |
Why Price-Only Comparisons Create Sourcing Risk
Price-only comparisons create sourcing risk because quotations can contain different assumptions about material, setup count, tolerance interpretation, inspection, deburring, finishing, packaging, scrap, outside services, and delivery responsibility. A lower price can be valid when a supplier has a more efficient route, but the saving must be explainable against the same scope. Normalize revision, quantity, incoterm, material certification, surface state, inspection records, first-article requirements, tooling ownership, nonrecurring charges, and change rules before comparing totals. An omitted inspection step or unpriced finishing dependency is not a process improvement. Place unresolved assumptions in a comparison register and withhold the award until each candidate prices or rejects the same obligation.
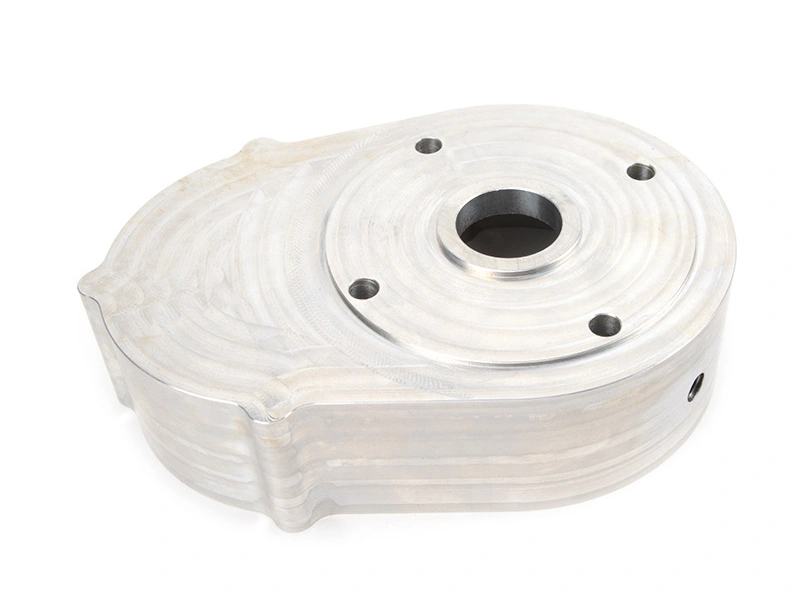
Consider a hypothetical 6061-T6 housing with a milled sealing face, a bored datum feature, a positional hole pattern, and anodizing after machining. The main failure modes are free-state movement after unclamping and dimensional change at bores or threads after finishing. A credible route roughs the part, controls the datum transfer, finishes critical features under stable conditions, defines masking, and inspects requirements in the specified final state. Validation may include free-state flatness after release, bore size and position after finishing, post-finish thread gauging, and a specified functional seal or assembly check. The buyer should reject a cheaper route if it relies on unrecorded hand correction or inspects only before anodizing. Production approval requires representative processing and documented acceptance, not one reworked sample.
How DFM, Engineering Response, and Delivery Capability Reduce Risk
DFM, engineering response, and delivery control reduce risk only when each produces a traceable decision rather than informal advice. A useful design-for-manufacturability proposal identifies the affected feature, technical cause, requirement at risk, proposed change, cost or schedule effect, and validation consequence. The buyer's functional owner then accepts, rejects, or revises the proposal, and the controlling drawing or deviation record captures the decision. Tool access, wall rigidity, thread depth, datum strategy, inspection access, and finishing allowance are valid discussion points, but no supplier should silently convert a DFM suggestion into a production change. Review the quality of the closure, not merely the number of comments.
Engineering response has value when it closes drawing conflicts and production assumptions before they enter the schedule. Track the question, owner, response date, technical resolution, affected documents, and open dependency. Delivery evidence should use the same discipline: a dated route, current constraint, outside-process commitment, buyer input date, escalation owner, and recovery condition. Response speed without an accurate answer can accelerate the wrong decision, while a polished schedule without material or inspection dependencies hides risk. The supplier is ready to advance when technical questions, route ownership, and schedule commitments agree in one controlled record.
Decision Control | Evidence to Request | Award Rule |
|---|---|---|
DFM review | Cause, affected requirement, proposal, approval, and validation impact | No production change without controlled buyer disposition |
Engineering response | Question log, owner, closure, and document revision | Advance only when technical assumptions are closed |
Delivery control | Dated route, constraint, dependencies, escalation, and recovery | Accept dates supported by owned process commitments |
Production planning | Representative route, release gate, and change-notice rules | Volume follows verified production-intent evidence |
How Buyers Should Make the Final Selection
Buyers should make the final selection with a gated scorecard that separates commercial value from technical and supply risk. Score geometry and material fit, characteristic-level quality evidence, usable constraint capacity, delivery ownership, DFM closure, production-stage readiness, and total comparable cost. Weight each category according to the consequence of failure rather than giving every row equal value. Some findings are stop conditions, not points to average away: an unresolved drawing conflict, unauthorized material substitution, unsuitable measurement method, concealed route change, unnamed outside process, or refusal to provide required change notice. A supplier can advance only when mandatory gates pass and any residual risk has a named owner, action, due date, and buyer-approved disposition.
The RFQ must give every candidate enough controlled information to produce a comparable technical response. Include the 2D drawing and 3D model, governing revision, units, material grade and condition, stock or traceability requirements, critical datums and GD&T, and final surface state. Add edge and burr requirements, cleanliness, quantity by stage, expected release pattern, inspection records, functional tests, packaging, delivery location, and approval requirements. State which document controls when the model and drawing conflict. Ask candidates to list assumptions, exclusions, proposed deviations, outside processes, lead-time dependencies, and buyer-furnished inputs. The final award record should show why the selected route passed each gate, not simply which quotation had the lowest total.
Conclusion
Evaluate CNC machined part manufacturers by the evidence behind quality, capacity, and lead time. The selected supplier should show a part-specific route, suitable material control, characteristic-level manufacturing and measurement logic, representative stage-gate results, constraint-based capacity, and owned delivery dependencies. Price, certificates, machine lists, and first articles remain useful inputs, but none proves the complete production system alone. The practical decision is to advance only the supplier whose documented route meets mandatory requirements and whose remaining risks have controlled dispositions.
Use the main CNC machining services page to confirm the available process family, then match release evidence to prototyping, low-volume manufacturing, or mass production. Send the controlled RFQ package with stage quantities, critical characteristics, final-state acceptance, required records, and delivery dependencies. Compare responses against the same stop conditions and release gates. That sequence lets procurement choose on verified process fit and recoverable supply risk while the service page remains the correct destination for capability and inquiry details.
FAQ
What Should Buyers Look for When Comparing CNC Machined Part Manufacturers?
Can CNC Machined Part Manufacturers Handle Both Prototype and Production Orders?
What Materials Should Good CNC Machined Part Manufacturers Be Able to Process?
How Do CNC Machined Part Manufacturers Control Quality and Consistency?
How Can Buyers Reduce Risk When Choosing CNC Machined Part Manufacturers?