How do titanium and aluminum anodizing differ in function and film structure?
Titanium anodizing forms a thin, dense TiO₂ interference film for color identification, biocompatibility, and corrosion support, while aluminum anodizing forms a thicker porous Al₂O₃ layer for wear resistance, dye absorption, and sealing. The two processes share the word anodizing, but they solve different engineering problems. A buyer should choose between them by material, required function, dimensional allowance, color method, cleaning requirement, and final inspection condition, not by finish name alone.
Film Structure and Formation Mechanism
The core difference is how each oxide grows and behaves in the electrolyte. For CNC Aluminum Anodizing, sulfuric acid anodizing commonly grows aluminum oxide while the acidic bath also dissolves part of that oxide. This competing growth and dissolution creates a porous cellular structure. Those pores are useful because they can accept dyes, hold sealing chemistry, and create a hard functional surface. The buyer must account for coating thickness on bores, threads, slots, and press-fit features because aluminum anodizing has measurable build-up and partial inward growth.
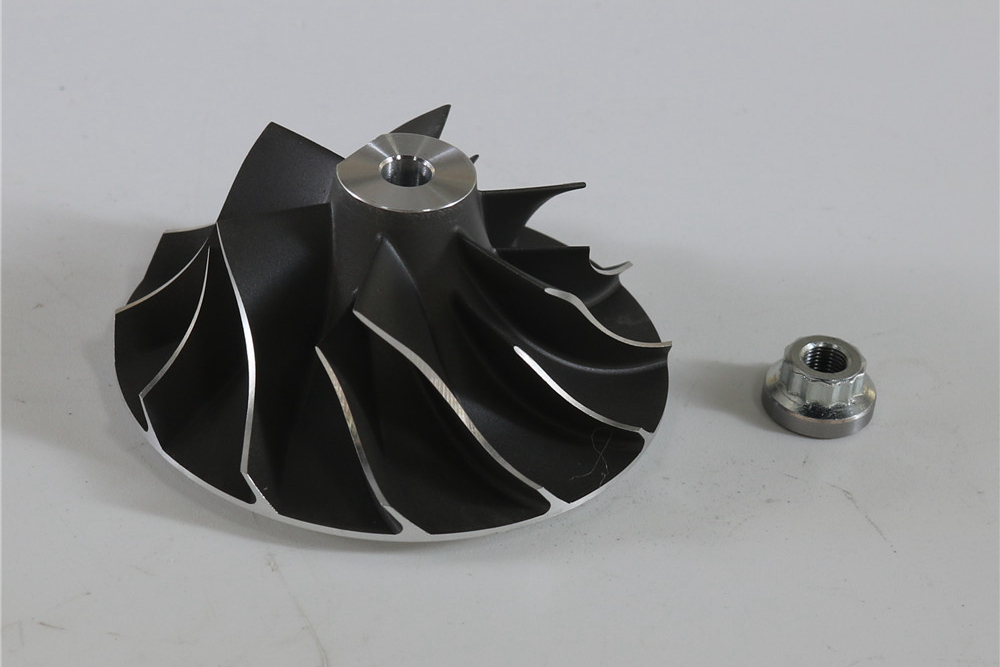
In contrast, titanium color anodizing usually forms a dense, non-porous titanium oxide film by voltage-controlled oxide growth. The visible color comes from thin-film interference, not pigment absorption. Light reflects from the outer oxide surface and the oxide-metal interface, and the oxide thickness changes the perceived color. The actual film for color anodizing is usually nanometer-scale rather than a thick wear coating. Surface preparation, cleaning, alloy condition, voltage control, and part geometry still matter because they influence color uniformity, surface cleanliness, edge condition, and whether shadowed areas anodize consistently.
Primary Functional Differences
This structural divergence decides the correct finishing function. Aluminum anodizing is often selected when the surface must become harder, more wear resistant, more corrosion resistant after sealing, or able to carry a dyed color. Titanium anodizing is usually selected when the part already uses titanium for strength, corrosion resistance, or biocompatibility, and the finish must add identification color or a controlled oxide surface without large dimensional change.
Aluminum Anodizing is a Functional and Decorative Workhorse: The thick, hard, and sealed anodic layer on aluminum is primarily for improved wear resistance, corrosion protection, and paint or adhesive adhesion. The porous structure is essential for its decorative function because it allows dye to enter the oxide before sealing. This makes the process useful for Consumer Products, housings, brackets, handles, panels, and industrial hardware that need durable color. The engineering risk is dimensional change. A bright finish on the outside can still be unacceptable if coating growth reduces a bore, tightens a threaded feature, or changes a sliding fit.
Titanium Anodizing is for Performance, Biocompatibility, and Aesthetics: The TiO₂ film is dense and chemically stable, supporting corrosion resistance and color identification without adding a thick coating. This is important for precision parts in the Medical Device industry, where foreign dyes may be undesirable and surface cleanliness can be part of the validation plan. Titanium anodizing can also help separate left/right parts, instrument sizes, or assembly groups by color. It is a common finish for Titanium CNC Machining Service parts when the drawing allows interference colors and the supplier controls cleaning, masking, contact marks, and post-finish inspection.
Comparative Table: Key Differences
Attribute | Aluminum Anodizing | Titanium Anodizing |
|---|---|---|
Oxide Layer | Typically micrometer-scale porous Al₂O₃; Type II sulfuric anodizing is often specified around 5-25 µm, while hard anodizing may be thicker when the drawing allows it. | Usually a thin, dense TiO₂ interference film for color anodizing; it should not be treated as a thick wear coating unless a special anodic process is specified. |
Color Mechanism | Dyes enter the porous oxide before sealing, so color depends on pore quality, dye chemistry, sealing, alloy, and surface preparation. | Color comes from voltage-controlled optical interference, so alloy condition, voltage, contact method, cleanliness, and viewing angle affect the result. |
Primary Function | Wear resistance, corrosion protection after sealing, decorative color, and improved adhesion when the aluminum design allows coating growth. | Color coding, biocompatible surface control, corrosion support, and identification on precision titanium parts with very small coating build-up. |
Dimensional Impact | Coating build-up can affect holes, threads, slots, fits, and masked surfaces; the drawing should define allowance and inspection after anodizing. | Color anodizing usually has minimal dimensional impact, but cleaning, polishing, masking, and contact marks can still affect functional edges or surfaces. |
Post-Process | Sealing is commonly required for dyed or corrosion-focused aluminum anodizing; poor sealing can change color durability and corrosion performance. | No dye sealing is normally used for color anodized titanium, but cleaning, handling, passivation compatibility, and validation requirements may still apply. |
Engineering Implications for Part Design
Select aluminum anodizing when the part is aluminum and the design needs a harder surface, dyed color, corrosion protection after sealing, or controlled adhesion. Select titanium anodizing when the part is titanium and the drawing needs color coding, a clean oxide surface, biocompatibility support, or very low dimensional build-up. The RFQ should state alloy, temper or grade, finish class, target color, masked areas, critical dimensions after finish, required certificates, and whether inspection is before or after anodizing. For stainless or plated parts, Stainless Steel Passivation or Electroplating Service may be better choices. The safest procurement decision is to specify the material and final function first, then choose the surface process that protects that function without creating new tolerance, cleaning, or validation risk.